Tracegrow is a Finnish cleantech company that recovers manganese and zinc from recycled alkaline batteries and
industrial side streams, providing high-purity circular raw materials for the agriculture and battery industries.
At its Kärsämäki facility in Finland, Tracegrow produces manganese sulphate for the fertilizer industry. The process produces a manganese solution from which a precipitate containing silver among other substances is separated before further processing of the final product. The fine precipitate is challenging to filter, making efficient solid-liquid separation a critical factor in ensuring product
quality.
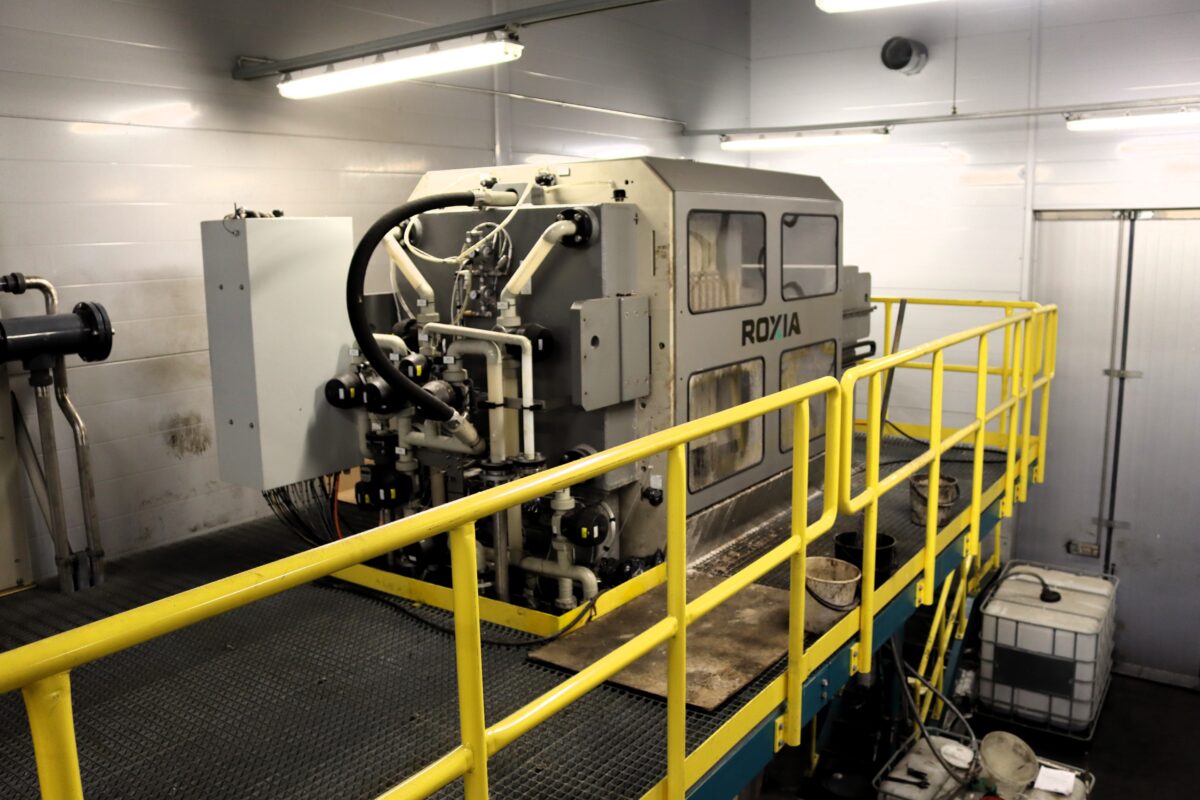
In 2023, Tracegrow commissioned a Roxia Smart Filter Press (SFP), a fully automated filter. Based on operational experience, the filter has met expectations and delivered reliable performance in this demanding application.
Roxia Selected After Comparing Several Alternatives
When Tracegrow was looking for a filtration solution for separating a precipitate, technologies from several leading suppliers were evaluated. The decision was based on both technical performance and the practicality of cooperation throughout the project.
The Roxia SFP filter was selected due to its competitive pricing, process suitability, and the availability of local Finnish-language support.
Integrating the filter into the customer’s existing systems required some customization, but the project progressed according to plan and the filter was successfully incorporated into the process.
Reliable Performance in a Demanding Application
For Chempolis, one of the most important requirements is the ability to produce sufficient volumes of lignin for customers. Before the introduction of the Roxia SFP, the pilot plant relied on rented equipment.
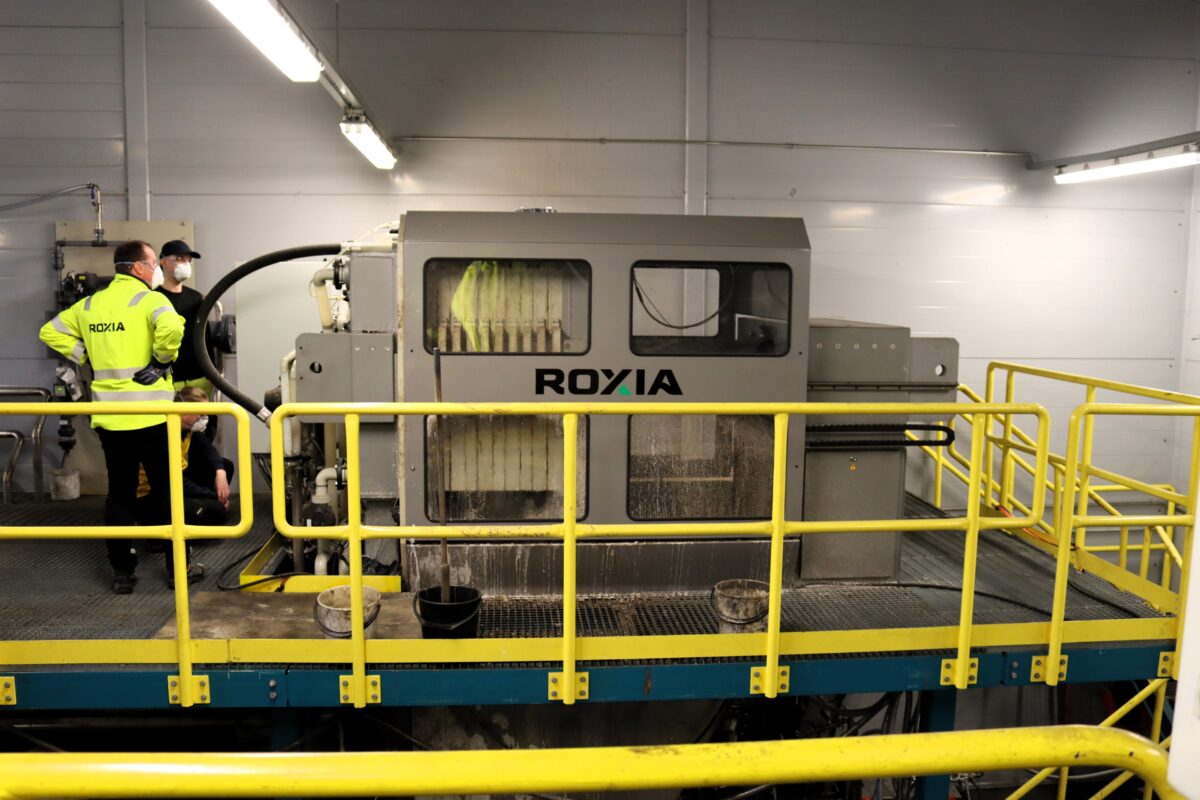
The slurry processed by the filter is challenging from a filtration perspective, but the Roxia SFP has performed well and fulfilled the expectations set for it.
“We would choose the Roxia SFP filter again. The unit has performed well, and any challenges we have encountered have been
related more to the filter feed material than to the filter itself,” says Jonni Fagerroos, Maintenance Engineer at Tracegrow
Kärsämäki.
Filtration performance has met the required targets, and the resulting manganese sulphate solution has been of high quality. Turbidity sensors have operated reliably, supporting process control and consistent product quality. The filter’s automated monitoring and diagnostic features have also contributed to operational reliability in this demanding
application.
Based on operating experience, maintenance requirements have remained low. No spare parts have been needed since commissioning, and no significant equipment-related issues have been encountered. The filter is typically operated in batch mode four to five times per week as part of the production process.
Easy-to-Use Solution for Daily Operation
The filter has proven straightforward to operate, and new users have been able to learn its use quickly. Thanks to its fully
automated operation, the filter requires minimal operator involvement during normal production.
“There have been no problems with the Roxia filter. Any challenges have been related to the process and the material being
filtered, not to the equipment itself,” says Fagerroos.
Routine maintenance activities have been considered simple and straightforward. Users noted that a troubleshooting
checklist could be a useful addition when investigating potential process disturbances.
Since commissioning, the filter cloths have not required replacement. Over time, filtration cycles have become slightly
longer due to the natural blinding of the cloths, which is a normal phenomenon in this type of application. In such cases,
the addition of a cloth washing system could be a beneficial way to further optimize the process.
Cooperation Supports Process Development
Tracegrow has been satisfied with the support provided by Roxia after commissioning. Roxia’s expertise has been
particularly valuable when addressing challenges related to the broader process rather than the filtration equipment itself.
The customer also sees potential in utilizing Roxia’s remote monitoring solutions to support future operation and
troubleshooting.